
Nonwoven fabrics are classified by how the web is formed and how its fibers are bonded, and three processes dominate: spunbond (strong, economical structure), meltblown (ultra-fine fibers for filtration), and spunlace (soft, cloth-like feel for skin contact). As defined by ISO 9092 and the industry associations INDA and EDANA, a nonwoven is an engineered sheet of fibers or filaments given its structural integrity by physical or chemical bonding rather than by weaving, knitting, or papermaking — so the way the web is formed and bonded is, quite literally, what defines each type. A fourth term you’ll meet constantly — SMS — is not a process but a sandwich of spunbond and meltblown layers. This guide explains how each type is made, what it’s good at, and how to match a type to your product. For the fundamentals of what makes a fabric “nonwoven” in the first place, start with our guide to what nonwoven fabric is.
What Is Spunbond Nonwoven?
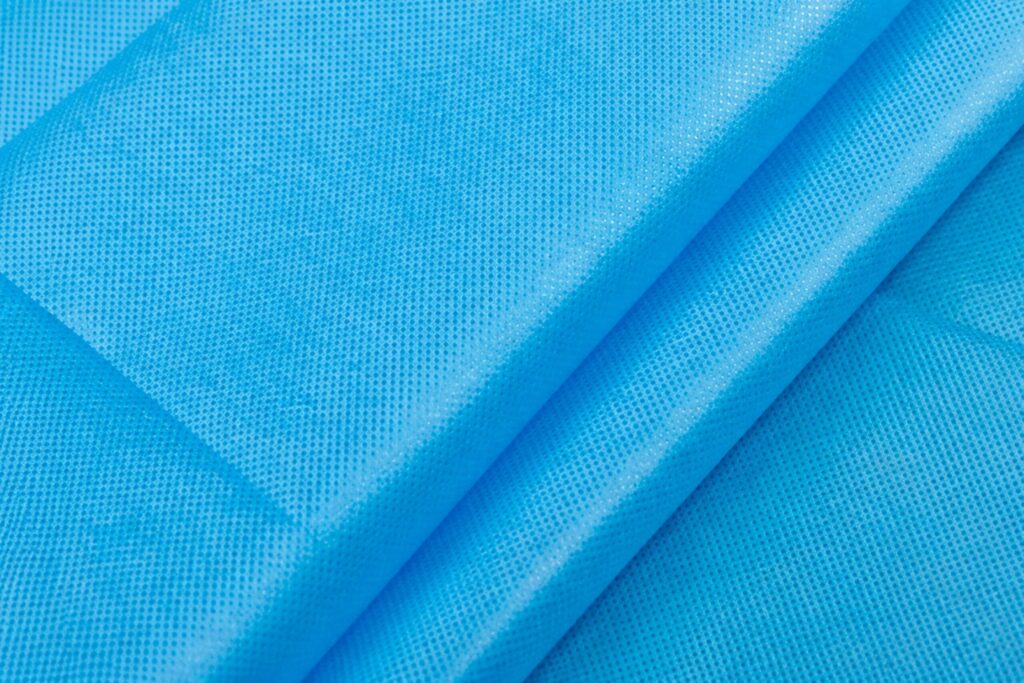
Spunbond is made by extruding continuous thermoplastic filaments (typically 15–35 μm in diameter), laying them into a web, and bonding them — usually with heated rollers. Continuous filaments give spunbond its signature property: strength.
- Strengths: high tensile strength, abrasion resistance, low cost at scale.
- Limits: relatively coarse hand-feel; limited filtration on its own.
- Typical uses: the outer layers of medical masks and gowns, agriculture covers, shopping bags, furniture and bedding substrates.
What Is Meltblown Nonwoven?
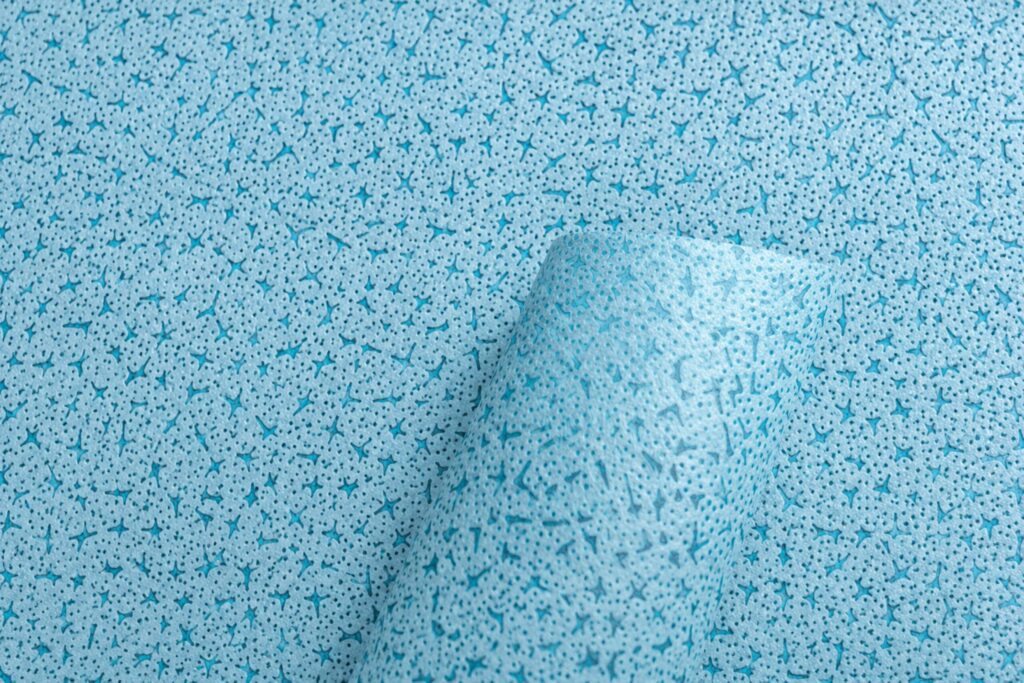
Meltblown extrudes molten polymer through fine nozzles into high-velocity hot air, shattering it into microfibers as fine as 0.5–5 μm that self-bond as they cool. Those ultra-fine fibers create a dense web with enormous surface area — the basis of filtration.
- Strengths: outstanding particle and bacterial filtration, good barrier properties, soft and fluffy.
- Limits: low mechanical strength, poor abrasion resistance — meltblown almost never works alone.
- Typical uses: the electrostatic filter layer in medical masks and respirators, liquid filtration media, oil absorbents.
This is why a medical face mask is a three-layer design: spunbond outside for strength and splash resistance, meltblown in the middle doing the filtering, and a soft bonded layer against the skin.
What Is Spunlace (Hydroentangled) Nonwoven?
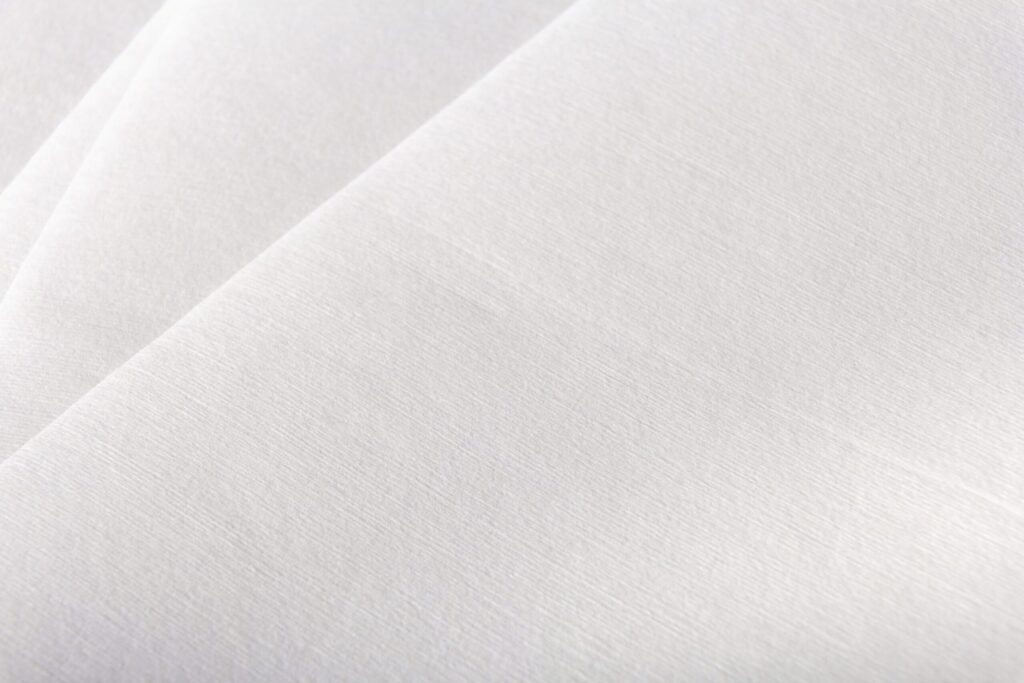
Spunlace — also called hydroentangled fabric — uses high-pressure water jets instead of heat or glue to tangle fibers together. Because nothing melts or glues the fibers stiff, spunlace keeps a textile-like drape and softness that other nonwovens can’t match, and it blends natural, regenerated, and synthetic fibers freely (cotton, viscose, polyester).
- Strengths: soft, absorbent, low-linting, cloth-like feel; excellent for skin contact.
- Limits: lower strength than spunbond; cost above commodity spunbond.
- Typical uses: wet wipes, disposable face towels, sheet mask substrates, medical and cosmetic wipes.
For how spunlace is made, which fibers and patterns it comes in, and how buyers specify it, see our spunlace nonwoven guide.
What Is SMS — and Why Is It Everywhere?
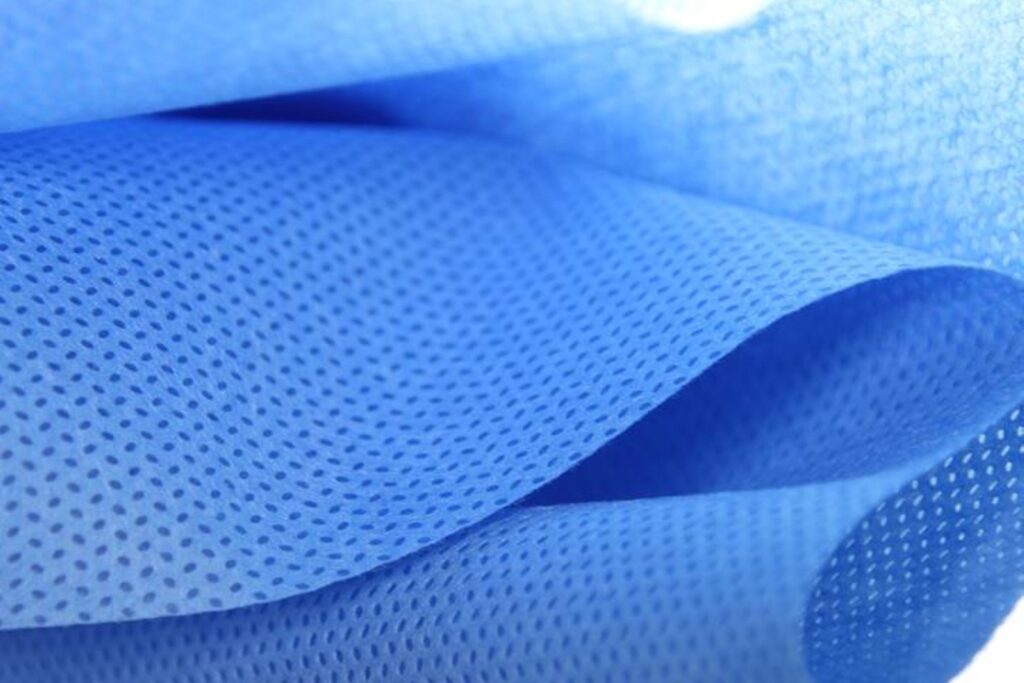
SMS stands for spunbond–meltblown–spunbond: two strength layers wrapping a filtration layer. The composite gets spunbond’s durability and meltblown’s barrier in one fabric — which is why SMS dominates surgical drapes, gowns, and sterile packaging. Variants (SMMS, SSMMS) tune the ratio of strength to barrier by adding layers. For how the two layer types differ and why SMS stacks them, see our guide to how spunbond and meltblown layers compare.
Other process routes you may encounter: thermal bonded (soft, used against skin, e.g., mask inner layers), needle-punched (thick, felt-like, for geotextiles and padding), and airlaid (bulky and absorbent, for hygiene cores). They matter in specific niches, but spunbond, meltblown, spunlace, and SMS cover most sourcing conversations.
What About Needle-Punched and Airlaid Nonwovens?
Two further types show up in industrial, hygiene, and tabletop sourcing. Neither competes with spunlace or spunbond for the same jobs, but buyers should recognize them on a spec sheet.
Needle-punched nonwoven
Needle-punched (needlefelt) fabric is bonded mechanically: a carded web of staple fibers is run under a board of barbed needles that punch through the web thousands of times per minute, dragging fibers vertically until they lock together. No heat, water, or binder is needed, so almost any fiber works — polyester, polypropylene, wool, or recycled blends. The result is thick, felt-like, dimensionally stable, and typically the heaviest of the common nonwovens. Typical uses are geotextiles, automotive carpet and trunk liners, filter felts for dust collection, padding and insulation, and synthetic leather substrates.
Airlaid nonwoven
Airlaid fabric is formed from very short fibers — mostly fluff pulp (cellulose), sometimes with synthetic fibers — dispersed in an air stream and deposited onto a moving screen, then bonded with latex, thermal bonding through bicomponent fibers, or a combination of both. Because the fibers lie randomly in three dimensions, airlaid is bulky, lofty, and highly absorbent while staying softer than paper of the same weight. Typical uses are absorbent cores and acquisition layers in hygiene products, premium tabletop napkins, food-tray pads, medical underpads, and heavy-duty household wipes.
Side-by-Side Comparison
| Spunbond | Meltblown | Spunlace | SMS | |
|---|---|---|---|---|
| Fiber diameter | 15–35 μm | 0.5–5 μm | Fiber-dependent | Composite |
| Bonding | Thermal/calender | Self-bonding airflow | Water jets | Layered |
| Strength | High | Low | Medium | High |
| Filtration/barrier | Low | Highest | Low | High |
| Softness / hand-feel | Coarse | Soft but fragile | Most cloth-like | Medium |
| Relative cost | Low | Medium | Medium–high | Medium |
| Signature use | Structure & covers | Filter media | Skin-contact wipes | Medical barrier fabrics |
Spunlace vs Spunbond: What's the Difference?
The short answer: spunlace is bonded with water jets and behaves like cloth; spunbond is bonded with heat and behaves like a strong, papery sheet. That difference in bonding — together with staple fibers versus continuous filaments — explains almost every trade-off between them.
- Fiber form: spunlace uses short staple fibers (viscose, cotton, polyester, lyocell) that can be blended; spunbond uses continuous synthetic filaments, usually polypropylene or polyester.
- Feel and drape: spunlace is soft, flexible, and low-linting; spunbond is crisp, stiffer, and carries a visible embossed bond pattern.
- Absorbency: spunlace with cellulose fibers absorbs readily; untreated spunbond repels water unless a hydrophilic finish is applied.
- Strength: spunbond wins on tensile strength and abrasion resistance at the same basis weight.
- Cost: spunbond is the lower-cost commodity; spunlace costs more because of staple fiber prices and the energy needed for hydroentangling and drying.
In practice the choice is rarely a toss-up. Anything that touches skin repeatedly — wet wipes, baby dry wipes, facial towels, sheet masks — is typically specified as spunlace. Anything that must cover, carry, or protect at the lowest cost per square meter — bag bodies, mattress and furniture substrates, the outer layers of gowns and masks — is typically specified as spunbond.
Which Nonwoven Type Fits Each Application?
Most sourcing questions start from the product, not the process. The table below maps the six types covered above to the applications buyers ask about most; a check mark means the type is a standard choice for that job, and a note means it plays a supporting or niche role.
| Application | Spunlace | Spunbond | Meltblown | SMS | Needle-punched | Airlaid |
|---|---|---|---|---|---|---|
| Wet & dry wipes | ✓ standard | — | Oil and solvent wiping cloths | — | Heavy industrial wiping | Bulky household wipes |
| Medical drapes & gowns | Some reinforced gowns | Basic low-risk gowns and covers | Barrier layer inside SMS only | ✓ standard | — | Absorbent zones on drapes |
| Face mask layers | Optional skin-side layer | ✓ outer and inner layers | ✓ filter layer | — | — | — |
| Hygiene topsheet (diapers, pads) | Premium cotton-feel topsheets | ✓ standard (hydrophilic-treated) | — | Leg cuffs, not topsheet | — | Core and acquisition layer below the topsheet |
| Filtration | Some liquid filters | Support and pre-filter layer | ✓ standard (air and liquid) | Combined filter-support media | ✓ filter felts, dust bags | — |
| Packaging & sterile wrap | — | ✓ bags, covers, wraps | — | ✓ sterilization wrap | Protective padding | — |
Two rows deserve a closer look because the layering matters. For surgical use, our guide to surgical drapes explains why SMS, aperture, and towel drapes are built differently, and our breakdown of what medical masks are made of shows how spunbond and meltblown share the work in a 3-ply mask. For wiping tasks in controlled environments, low-lint constructions such as low-lint dry wipes are specified by particle release rather than by fabric type alone.
How Do You Choose the Right Type?
Work backwards from the job the fabric must do:
1. Touching skin repeatedly? → Usually spunlace (softness, absorbency, low lint).
2. Filtering air or liquid? → Meltblown — but plan a supporting layer for strength.
3. Need strength and a barrier? → SMS composite.
4. Structure, coverage, economy at scale? → Spunbond.
5. Harsh solvents or cleanroom duty? → Purpose-built low-lint constructions; see our cleanroom wipers guide for that specialized branch.
Basis weight (GSM), fiber blend, and finishing treatments tune each type further — the same process at a different weight behaves like a different material. When a product needs properties that no single type delivers, custom development is the answer: Graminton’s nonwoven material research center develops application-specific constructions from fiber selection up.
FAQ
Which is stronger, spunbond or meltblown?
Spunbond, by a wide margin — its continuous filaments resist tearing and abrasion, while meltblown’s microfibers prioritize filtration over strength. That’s why they’re usually combined rather than compared.
Is SMS a type of nonwoven fabric?
Strictly, SMS is a composite of two nonwoven types: spunbond skins around a meltblown core. It’s specified like a fabric type in practice because it behaves as one — strong, fluid-resistant, and breathable.
Why is spunlace preferred for skin-contact products?
The water-jet bonding leaves no melted bonding points or chemical binder, so the fabric stays soft, drapes like cloth, and can blend cotton or viscose for absorbency — ideal for face towels, wipes, and sheet masks.
Can different nonwoven types be combined in one product?
Constantly — that’s the norm, not the exception. A medical mask stacks two or three nonwoven types across its three layers; an SMS drape laminates two. Composite design is where most nonwoven innovation happens.
How can I tell spunlace from spunbond by hand?
Three quick checks work without a lab. Feel and drape: spunlace folds and drapes like a cloth napkin; spunbond feels crisp and papery and springs back. Look against the light: spunbond shows a regular embossed bond pattern (dots or diamonds); spunlace shows a random fibrous texture, sometimes with a fine apertured mesh pattern from the water jets. Water drop: a drop soaks into viscose or cotton spunlace almost immediately, while it beads on untreated polypropylene spunbond. When you tear them, spunlace leaves a fuzzy, fibrous edge; spunbond tears with a cleaner edge and a slight crackle. For a definitive answer, check the supplier’s spec sheet or have a lab examine the fabric structure under magnification.
Which nonwoven type costs more and why?
At a comparable basis weight, spunbond is usually the lowest-cost type: polymer goes from pellet to fabric in one continuous step at high line speeds. Meltblown costs more per kilogram than spunbond because throughput is slower and the fibers are far finer, but it is used in thin layers, so its share of a finished product’s cost stays moderate. Spunlace generally sits highest among the three because staple fibers such as viscose and cotton cost more than polypropylene, and hydroentangling plus drying consumes more energy. SMS lands between spunbond and spunlace depending on its meltblown ratio. Needle-punched and airlaid are priced mainly by fiber content and weight rather than by process. Across all types, fiber choice and basis weight move the price more than the bonding method does — which is why sampling two adjacent weights is a better cost lever than switching process.
Not sure which nonwoven fits your product? Tell us the application, target feel, and volume — our material R&D team will recommend constructions and send swatches.